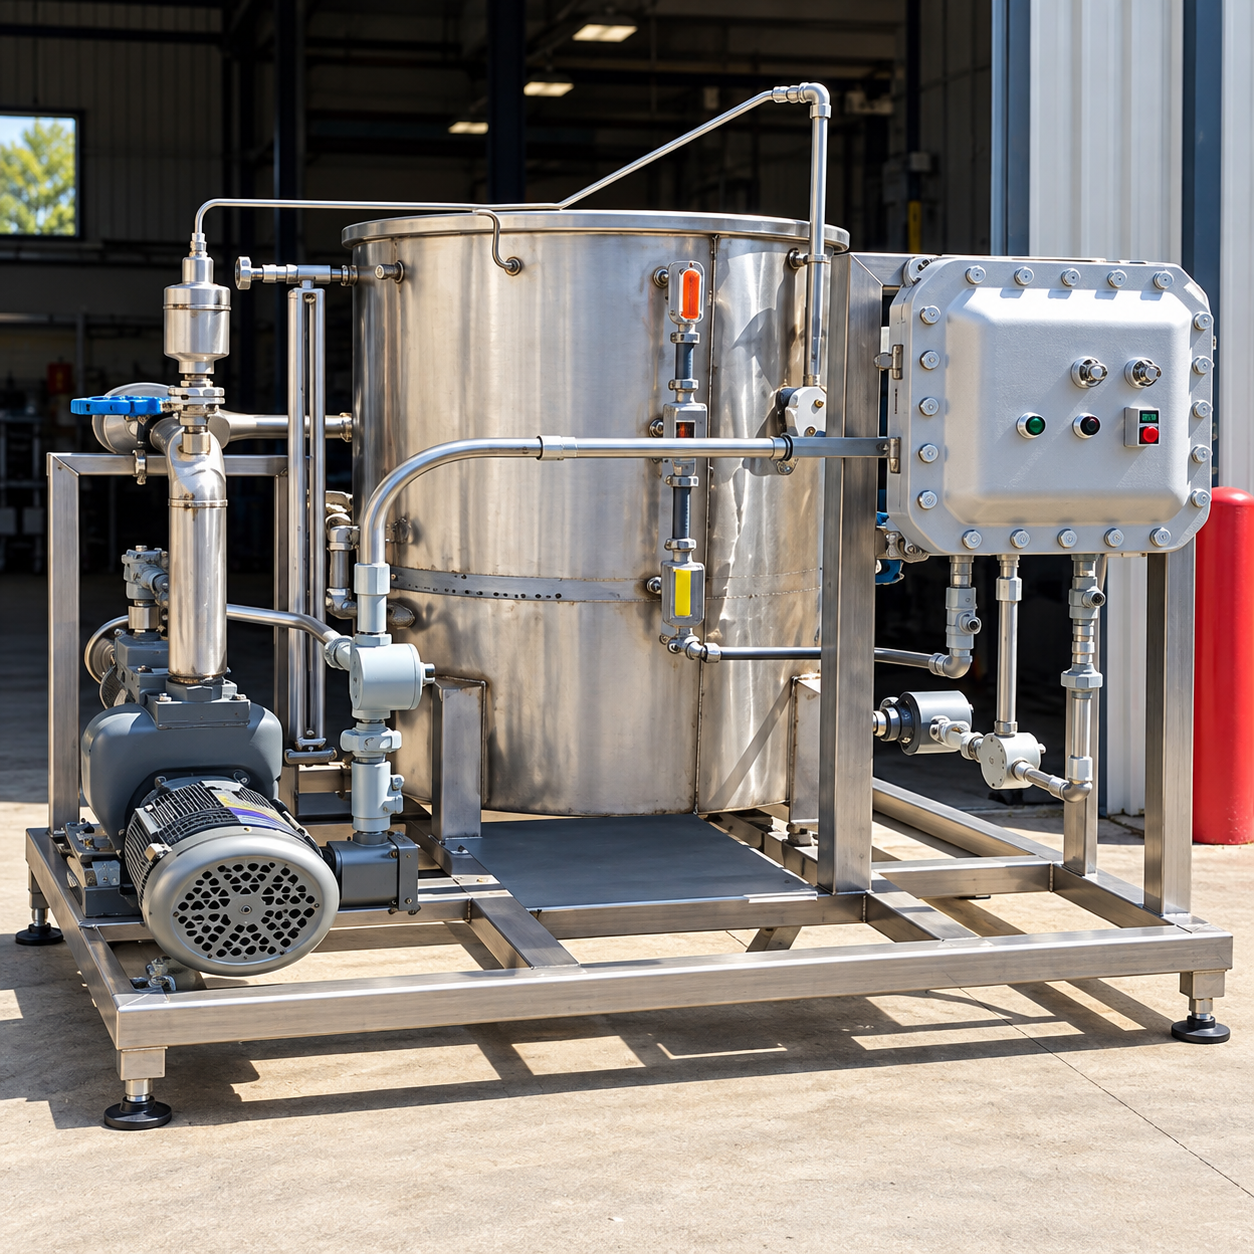
Fuel Recovery Systems
Stop throwing away good fuel. Schultz recovery units collect the product drained from sumps, filters and quality checks, and hold back water and sediment so it isn’t returned to storage.
- Sizes from 10 to 300 US gallons (38–1,136 L), or custom
- Nothing mechanical inside the tank to fail
- No sediment discharged back into storage
- Suited to cold climates – no freeze concerns
Description
Units available in several models to fit your size, budget and project scope.
Every day on an airfield or fuel depot, product is drawn off for quality control, from storage-tank and filter-vessel sumps, pipeline drain points and vent points, from samples taken when a delivery arrives and membrane filtration tests, and whenever filter elements are changed. Much of that fuel is perfectly usable, yet it often ends up as waste. A fuel recovery system captures it in a dedicated tank so it can be reclaimed in line with your quality procedures, cutting fuel losses and the cost of disposal.
Schultz units are designed so that contaminants stay where they belong. The tank contains no internal valves or moving parts that could fail or trap dirt, and the design prevents collected sediment being discharged back into storage. Because there’s no risk of a valve being left open by mistake, operation is safer too.
The system also copes with harsh weather: it’s designed to operate in sub-zero conditions without the freezing problems that can affect water-laden recovery tanks. Units are engineered and fabricated in the USA and suit aviation fuels as well as other fuel and oil storage applications.
Standard Sizes:
10-Gallon 100-Gallon
20-Gallon 200-Gallon
55-Gallon 300-Gallon
*Custom Sizes Available
Applications:
- Tank sumps
- Filter sumps
- Low point drains
- High point vents
- Samples from fuel truck receipts
- Membrane filtration tests
- Drained fuel from filter change outs
- Used in Aviation and non-aviation
Not all recovery units are created the same.
What sets Schultz apart?
- Made in the USA by experienced engineers, machinists, fabricators.
- Safer operation with no worry about inadvertently leaving the valve open.
- No contamination or sediment discharge back into storage.
- Works in cold climates without freeze concerns.
- No valves or mechanisms inside the tank.
Shipping Information
Customised or made-to-order products may require additional time for assembly, testing and preparation before dispatch. In-stock items are available for next-day delivery.
As lead times can vary depending on your chosen product specifications, please contact us for an estimated dispatch and delivery time before placing your order if timing is important.
Installation & Post Installation Services Available – 50% off for the 1st After Installation Services
Our certified engineers provide nationwide installation, calibration and ongoing maintenance for selected products in our range.
Book installation with your order and receive 50% off your first post-installation service visit. Speak to an engineer for details. Call 0345 230 7887 or email sales@bms-ltd.com.


Complete Liquid System Solution

CompEx Electrical Services

DSEAR Risk Assessments

Environmental Audits and Surveys UK

Flow Meter Calibration

Flow Meter Installation

Flow Meter Refurbishment

Flow Meter Repairs and Maintenance

Flow Meter Services – Avery Hardoll

Flow Meter Services – Isoil

Flow Meter Services – Liquid Controls

Flow Meter Services – SATAM
